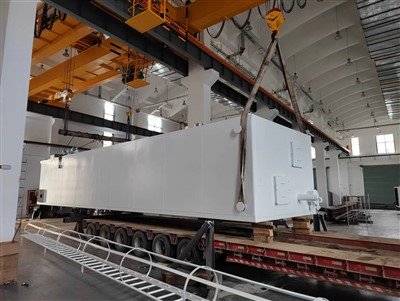
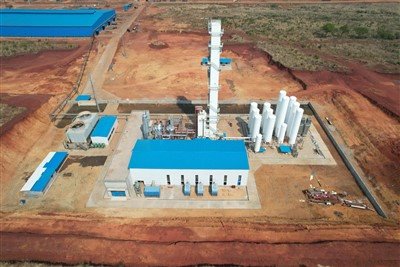
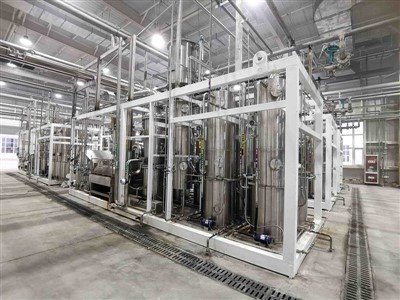
A cryogenic air separator plant (CASP) is a high-efficiency industrial system that liquefies and separates ambient air to produce stable, high-purity nitrogen, oxygen, argon, and specialty gases for semiconductor, medical, petrochemical, and photovoltaic industries. Consistent gas purity relies on professional feed air pretreatment with PSA equipment, precision low-temperature distillation, DCS intelligent automatic control, flexible load management, and proactive maintenance and air separation plant reconstruction. As a reliable global CASP supplier, HANTURBO delivers energy-saving, high-argon-recovery cryogenic air separator plants with full ISO certifications, customized industrial gas solutions, and complete overseas installation and after-sales services for international buyers.
In high-precision industrial sectors including semiconductor manufacturing, medical oxygen production, petrochemical processing, new energy photovoltaics, and food preservation, stable supply of high-purity industrial gases has become a core prerequisite for standardized production. Even minor fluctuations in gas purity, pressure, or output continuity can lead to defective products, production line shutdowns, or inflated operational costs. As the most reliable mainstream solution for large-scale and ultra-high-purity gas production, the cryogenic air separator plant (CASP) has become indispensable core equipment for global industrial enterprises. Unlike small-scale PSA gas generation equipment, a cryogenic air separator plant realizes deep liquefaction and fractional distillation of ambient air, stably producing high-purity nitrogen, oxygen, argon, and rare gases. It can meet industrial-grade, medical-grade, and electronic-grade ultra-high-purity gas standards, making it the top choice for overseas buyers looking for consistent, bulk gas supply. This article systematically analyzes the core technical logic of CASP stable operation, key anti-fluctuation design strategies, and professional supplier selection criteria, providing practical reference for global industrial purchasers evaluating a cryogenic air separator plant for their site.
The stable operation of any cryogenic air separator plant is built on precise multi-stage process control, covering feed air pretreatment, low-temperature heat exchange, high-precision distillation, intelligent automatic adjustment, and terminal storage and delivery. Each link adopts layered anti-interference design to cope with complex variable factors such as ambient temperature changes, air humidity fluctuations, and production load adjustments in different countries and climates. The first core guarantee of stable quality is scientific feed air preparation technology. Ambient air contains dust, moisture, carbon dioxide, and other impurities; if not completely removed, these impurities will freeze and block distillation towers and heat exchange equipment in low-temperature environments, causing irreversible fluctuations in gas purity. Professional CASP systems are equipped with multi-stage filtration and purification systems. This standardized pretreatment process eliminates impurity surge risks from the source and lays a solid foundation for long-term stable operation of the subsequent low-temperature distillation links of your cryogenic air separator plant.
The low-temperature distillation link is the core of CASP gas separation, and its stability depends on ultra-precise temperature and pressure control. The system cools the pretreated clean air to a liquefaction state of nearly -180°C, and separates air components through multi-stage distillation towers with different pressure levels. Nitrogen, oxygen, and argon with different boiling points are stratified and purified in the tower body to form independent high-purity gas streams. Advanced cryogenic air separator plant configurations adopt finned aluminum alloy heat exchangers with self-cleaning functions and high-precision flow control valves, which can dynamically adjust compressed air flow and cooling efficiency in real time according to external environmental changes. Whether it is extreme high temperature in summer or low temperature in winter, the system can maintain a stable heat transfer pinch point, avoid uneven distillation caused by temperature deviation, and ensure that gas purity does not drift with environmental changes. In addition, the independent argon recovery tower design optimizes the argon separation process, effectively improving the comprehensive gas yield and resource utilization rate while ensuring separation accuracy.
Intelligent monitoring and automatic adjustment systems are the key to long-term consistent operation of modern CASP equipment. Traditional old-fashioned air separation units rely on manual detection and adjustment, which has obvious delays and human error risks, making it difficult to meet ultra-high-purity gas production standards. New-generation
cryogenic air separator plant units are equipped with DCS distributed control systems, which monitor hundreds of core parameters such as gas flow, tower pressure, operating temperature, and terminal gas purity in real time all day long. Once any parameter deviates from the set standard, the system will automatically adjust the distillation reflux rate, air intake volume, and cooling load, and quickly correct purity fluctuations. For example, for semiconductor-grade 6N (99.9999%) ultra-high-purity gas production, the intelligent system can lock the purity error within 0.0001% for a long time, fully meeting the strict production requirements of very large-scale integrated circuits. This highly automated design not only ensures product stability but also reduces manual operation costs and improves the overall operational efficiency of the production line. For buyers who need flexible gas supply without sacrificing consistency, specialized nitrogen generation unit designs can be integrated with the cryogenic air separator plant, paired with buffer tanks that hold excess gas during low demand. These tanks act as a safety net, ensuring a steady flow of pure gas even during rapid demand spikes.
Proactive maintenance and flexible load management are essential supplementary strategies to maintain CASP performance stability. Long-term continuous operation will inevitably cause slight wear of equipment components and residue accumulation inside the tower body, which will gradually reduce separation efficiency and gas purity if not maintained regularly. Professional operation and maintenance mechanisms include regular replacement of filter elements, leak detection of control valves, regular flushing of distillation towers, and upgrading of aging components. For aging air separation units, professional air separation plant reconstruction and energy-saving upgrading services can effectively restore equipment performance, improve argon recovery rate and energy-saving level, and extend equipment service life at a fraction of the cost of purchasing a brand-new cryogenic air separator plant. Many overseas customers find reconstruction services particularly cost-effective when their existing CASP still has usable pressure vessels and pipe frameworks but suffers from outdated control systems or degraded heat exchangers.
Terminal storage and transportation management is the final line of defense for gas quality stability. High-purity gas separated by distillation may be contaminated by external air or mixed with impurities during storage and transmission without professional protection. High-quality cryogenic air separator plant supporting systems adopt fully sealed pressure pipelines and professional cryogenic liquid storage tanks. The heat insulation and pressure stabilization design of the storage tanks prevents low-temperature liquid gas from evaporating and mixing with air, while the terminal pressure regulator ensures stable and consistent gas delivery pressure. For enterprises with limited plant space, supporting gas supply station solutions can also be customized to realize centralized gas storage and stable delivery, ensuring zero contamination of terminal gas products.

When global purchasers choose a cryogenic air separator plant supplier, technical strength, product certification, R&D innovation capability, and overseas service capacity are the core evaluation indicators. HANTURBO Technology (Zhejiang) Co., LTD, a professional air separation and special gas equipment manufacturer founded in 2012, has outstanding comprehensive advantages in CASP R&D, manufacturing, customization, and after-sales service, and is a reliable partner for global industrial gas equipment procurement. The company is located in Huzhou, Zhejiang, China, within the Shanghai metropolitan circle, only 200km away from Shanghai Port and Ningbo-Zhoushan Port, with superior logistics conditions, which can efficiently meet the transportation and delivery needs of overseas cryogenic air separator plant orders.
Focusing on the field of gas equipment for more than a decade, HANTURBO integrates independent design, precision manufacturing, on-site installation, commissioning, and full-cycle maintenance services. Its core product line covers cryogenic air separation plants, special gas purification equipment, natural gas liquefaction equipment, CO₂ liquefaction systems, and cryogenic liquid storage tanks, fully covering the gas equipment needs of metallurgy, petrochemical, medical, environmental protection, semiconductor, photovoltaic, and fertilizer industries. The company has established long-term in-depth technical cooperation with Zhejiang University, carrying out joint research and technological breakthroughs in ultra-high-purity electronic special gases and high-efficiency air separation technology. In June 2025, HANTURBO jointly established the Zhejiang University Specialty Gas & Equipment Innovation Team, successfully developing 6N-grade ultra-high-purity electronic gas production and purification systems including N₂O, BCl₃, 3MS, C₃H₆, C₄F₈, C₂F₆, and HBr, filling the domestic technical gap in high-end special gas equipment and solving the long-term import dependence problem of ultra-high-purity gas production equipment for semiconductor chip manufacturing.
In terms of air separation core technology, HANTURBO's cryogenic air separator plant has obvious industry advantages of high argon recovery rate and low energy consumption. Through optimized distillation tower structure design and intelligent control system upgrading, the equipment maintains stable high-precision separation efficiency under long-term full-load and variable-load operation, effectively reducing enterprise production energy consumption and operating costs. The company has complete advanced production equipment such as large plate rolling machines, automatic welding equipment, plasma cutting machines, and CNC precision processing equipment, with strict full-process quality control capabilities. All products have passed ISO9001 quality management system, ISO14001 environmental management system, ISO45001 occupational health and safety management system certifications, and hold special equipment production licenses, national high-tech enterprise certificates, AAA enterprise credit ratings, and a number of core technical patents, with qualified and reliable product quality.
In terms of overseas market service, HANTURBO has rich international project experience, and its cryogenic air separator plant, CASP equipment and gas system solutions have been successfully exported to Indonesia, Turkey, Mexico, India, Iran, Zimbabwe, Pakistan, Vietnam and many other countries and regions. The company provides one-stop full-cycle services for overseas purchasers, including pre-sales customized scheme design according to industry purity standards and production scale, factory precision manufacturing, professional on-site installation and commissioning, operator technical training, and long-term after-sales operation and maintenance support. For aging equipment of old customers, it also provides professional air separation plant energy-saving upgrading and reconstruction services, helping customers quickly restore equipment stability and improve production efficiency with low cost.
In conclusion, the stable performance of a cryogenic air separator plant is the result of the integration of precision process design, intelligent automatic control, proactive maintenance management, and professional terminal guarantee. For global industrial enterprises engaged in high-precision manufacturing and large-scale industrial production, choosing a high-quality CASP system and a powerful professional supplier is crucial to stabilizing product quality, reducing operating costs, and enhancing market competitiveness. With mature core technology, perfect certification system, rich overseas project experience, and comprehensive one-stop services, HANTURBO can provide global purchasers with customized, high-stability, energy-saving and efficient cryogenic air separator plant solutions and full-life-cycle technical support, creating long-term stable production value for overseas customers.
If you are ready to explore how a cryogenic air separator plant or related gas solutions can meet your quality and stability needs, our team is ready to help. We design, build, and maintain CASP systems that deliver reliable, high-purity gas products for customers across industries. Whether you need a full on-site cryogenic air separator plant, supplementary PSA equipment, or support for air separation plant reconstruction for your aging unit, we can provide tailored solutions. Get in touch today to discuss your gas production goals and find the right fit for your operations.